
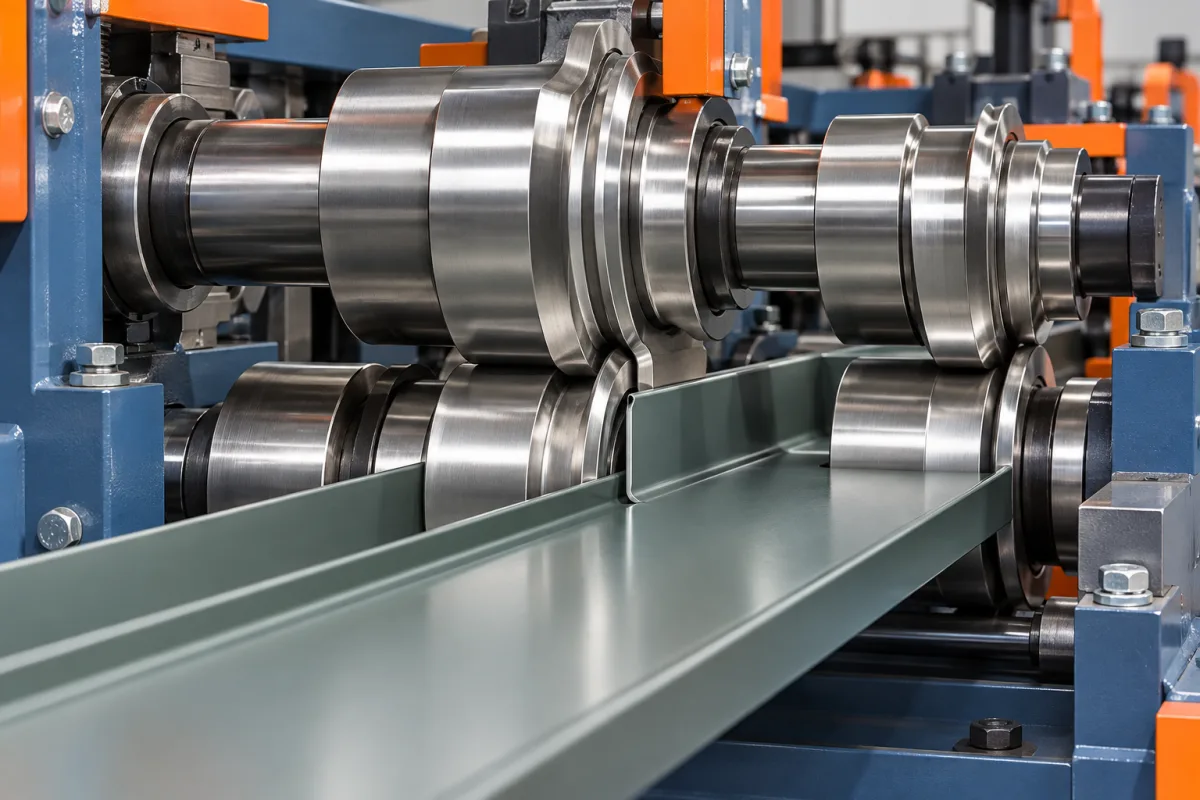
Standing seam tooling creates a matched pair of panel edges, not simply two raised ribs. Their hooks, returns and contact surfaces must work with the chosen attachment and closing method. Tooling review should therefore begin with the complete joint and follow it through forming, cutting and assembly.
Use open and closed seam drawings together
The open section defines what the panel former must deliver. The assembled section shows how those features work with the neighboring panel and attachment. Both are needed to identify functional dimensions and meaningful inspection references.
A nominal seam height or commercial profile name is insufficient. Two profiles can share those descriptions while having different returns and mating surfaces. Keep the tool specification tied to a controlled drawing revision and the correct assembly components.
Separate snap engagement from mechanical closure
A snap profile is designed around its specified engagement behavior. A mechanically closed profile follows a defined closing route after positioning. Their tooling requirements should not be assumed interchangeable merely because their finished seams look similar.
Some engineered profiles support alternative closing methods, but that capability needs explicit design evidence. Do not generalize it to unrelated seams. Ask which exact tool configuration and assembly procedure are approved for each intended product.
Review both edge developments as one system
Successive passes form the shoulders, hooks and returns. The relationship between the two edge paths and the connecting pan determines the complete section. Ask the tooling specialist to explain how the required geometry is developed in the intended material combinations.
Inspect the full panel rather than approving isolated edge coupons only. Pan width, edge position and straightness can affect assembly even when each local return appears plausible. The acceptance plan needs to capture those relationships.
Include clips and closing equipment in development
Supply the specified clips or fixing arrangement during tooling trials. Where mechanical closure is required, use the intended compatible seaming equipment and procedure. A substitute selected by nominal height can introduce a mismatch unrelated to the former's basic capability.
Record how the joint closes, not just its final photograph. Unusual resistance, incomplete engagement or local reshaping should be documented. These observations help determine whether the tools, material and mating components work together consistently.
Width adjustment is not universal seam flexibility
A line may change pan width while preserving one seam geometry. A new hook, return or attachment interface can require another tool set and related components. Request a configuration matrix distinguishing adjustment, change parts and unsupported products.
For each required change, identify how the first accepted panel is recovered. Guides, cutting parts and inspection references may change along with the main tools. A quoted adjustment time should not be mistaken for complete product changeover time.
Material behavior belongs in the tool approval
Provide grade or alloy, thickness convention, coating and strip width. The final geometry after forming can differ between materials, and the closing stage can reveal additional issues. Validate the combinations that will actually be produced rather than extrapolating from one demonstration coil.
Include surface inspection at the seam. A geometrically correct return is not the complete product if its finish is unacceptable after closure. Record the protective-layer condition and inspect by the agreed method so trial results can be reproduced.
Cut ends and long-panel support affect usable geometry
Review the cutting arrangement with the actual seam section. Inspect the ends for local distortion and compare them with the middle of the panel. A central coupon removed from a long sample can miss the feature that prevents installation from starting correctly.
Support during discharge also matters. Long panels should be inspected after the intended handling sequence. Tooling acceptance that ignores handling can leave uncertainty about whether later joint damage originated in forming, cutting or movement.
Curving and tapering need their own feasibility boundary
Do not treat a straight-panel tool set as automatic approval for curved or tapered work. The proposed route must explain how the changing geometry is produced and how the seam remains compatible. Additional equipment or a different process may be involved.
Provide the actual geometry and intended assembly, not just a visual concept. A curved roof image does not define panel development, seam behavior or material requirements. Keep any trial evidence specific to the product it demonstrates.
Validate repeatability after a real configuration change
Preserve the inspection datum scheme when comparing the initial and recovered panels. If the first sample is measured freely and the second is held against a fixture, an apparent improvement or deterioration may reflect the method rather than the tooling. The tool-delivery package should state how these checks were performed and identify the reference samples used during acceptance.
A meaningful flexible-tooling trial includes an initial accepted setup, a required change and a return to the original product. Inspect the open panel and assembled joint after recovery. This checks whether documentation and tooling references support repeatable production.
- Identify drawing, tools, material and attachment references.
- Measure pan and both seam edges on complete panels.
- Inspect cut ends and finish after handling.
- Assemble with the specified closing method.
- Repeat relevant checks after configuration recovery.
Frequently asked seam tooling questions
Can one final roll shape prove seam compatibility?
No. The complete forming development, material and mating components influence the result. Validate complete panels and their assembly rather than relying on the appearance of one tool.
Are equal-height seams interchangeable?
Not necessarily. Hooks, returns and clip contacts can differ. Use the exact section and joint revision when selecting tools and acceptance components.
Can a field seamer correct an incorrectly formed edge?
It should not be treated as a repair for an undefined profile error. The former must deliver the specified open section, and the closing equipment must follow the compatible system procedure.
What records should accompany a seam tool set?
Controlled profile and assembly drawings, tool identification, supported material combinations, setup references and acceptance results. Include the mating components and closing method used in the trial so later production can reproduce the approved condition.
Continue your research
- Standing Seam Roll Forming Machines
- Standing Seam Roll Forming Machine
- Snap Lock Standing Seam Machine
- 25mm Snap Lock Standing Seam Machine
- 38mm Snap Lock Standing Seam Machine
- 1 Inch Mechanical Lock Standing Seam Machine
- How Standing seam roll forming machine Works
- How To Choose a Standing seam roll forming machine
- Standing seam roll forming machine Price: What Affects the Cost?