
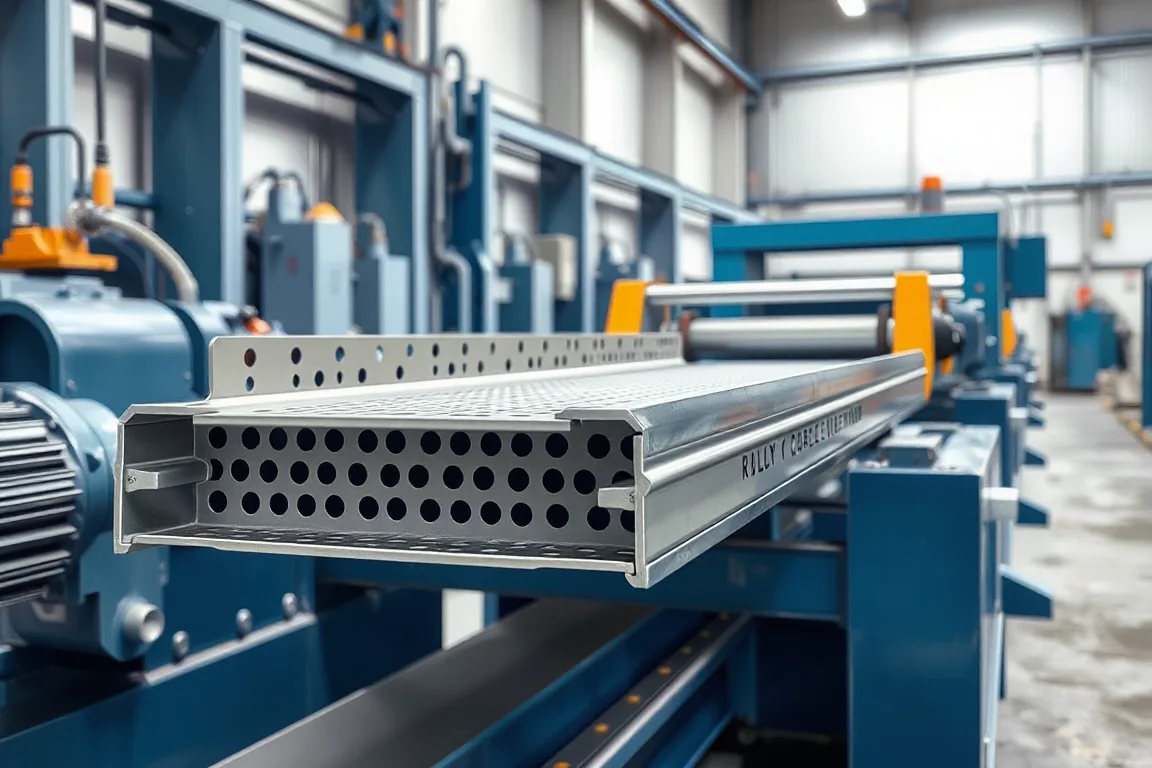
A GI cable tray roll forming machine processes the specified galvanized-steel tray product, but GI alone does not define a complete material or corrosion-protection specification. The buyer must state the steel grade, base-metal thickness and whether the tray is made from pre-galvanized strip or galvanized after fabrication. Those choices create different production routes.
The tray geometry remains equally important. Width, side height, returns, perforations and connection details determine the tools and accessory interfaces. A machine selected only because it is described as suitable for GI sheet may leave important product requirements unresolved.
Which galvanizing route is intended?
Pre-galvanized strip arrives with its specified coating before punching, forming and cutting. A post-fabrication route forms the component first and sends it through a separate coating process. The equipment and quality plan should identify the actual route rather than treat both as one finish.
Record the required delivered condition and who verifies it. The forming-line quotation should not imply that it includes a galvanizing plant unless that broader scope is explicit.
What material information is needed beyond GI?
State the steel grade, base-metal thickness, coating specification and incoming-strip requirements. Identify the thickness measurement convention so coating is not confused with the steel substrate. Pair this information with each tray size.
Use production-intent material during trials. Different grades, thicknesses and coatings can behave differently at bends and punched edges. Retain coil identity with accepted samples instead of treating every galvanized coil as equivalent.
Which tray geometry and features should be defined?
- Base width and side height with clear datums.
- Top return or cover-retention geometry.
- Solid or perforated base construction.
- Side patterns and end-coupling features.
- Required lengths and usable edge condition.
- Matching covers, couplers and fitting references.
A solid-bottom tray and a heavily perforated one may share a section while needing different feature equipment and trial conditions. Keep these variants distinct in the product matrix.
How does the forming route affect the coated surface?
The strip passes through guides, feature tools and progressive forming contact before cutoff. Inspect coating condition at bends and contact areas, and distinguish those observations from marks introduced during discharge. The actual material and surface requirements should guide acceptance.
Do not rely on a generic claim that galvanized material is maintenance-free or suitable for every environment. The required corrosion performance belongs to the selected product specification and application assessment.
What should be checked around punched and cut edges?
Define the acceptable edge condition and any specified downstream treatment. Check holes, slots, top returns and cut ends using the finished tray. Cable-contact areas and connection interfaces should remain usable after the full process.
Where the product is coated after fabrication, review the final inspection method with the coating process owner. Close accessory interfaces should be checked in the required delivered condition, not only before the final surface process.
How can sizes and material variants share a line?
Use a matrix linking tray geometry, input width, material and pattern. Identify adjustable dimensions and replacement tools. A line capable of changing base width does not automatically change side height or top-edge construction.
Demonstrate a transition that represents actual orders, including any coil change. Verify feature positions, cover fit and end connections after the adjustment. The first accepted finished tray is the useful changeover endpoint.
What should the packaging plan protect?
Protect the formed edges and specified surface condition during stacking and restraint. Define stack orientation and package identification for different coating routes or material grades. Similar-looking trays should remain traceable to the correct product.
Inspect a tray after normal bundle handling and fit its intended cover or coupler. This checks that packaging has not changed the return or side geometry. Keep wet-storage or other handling requirements within the material supplier's documented guidance rather than inventing a universal rule.
How should final-finish variants remain identifiable?
Use product codes that distinguish the substrate and protection route, not only tray width. A bundle of visually similar trays may have different material or finishing requirements. Check the label against the production record and a representative piece before release, especially where several finishing suppliers are involved.
What should the acceptance record include?
- Material and coating-route identity.
- Tray dimensions and top-edge geometry.
- Pattern and end-feature registration.
- Coating observations and agreed edge condition.
- Cover, coupler and fitting interfaces.
- Condition after final processing and packaging within scope.
- Accepted output for the stated size and material mix.
Keep dimensional acceptance distinct from product loading, electrical continuity and corrosion assessments. Each requires the appropriate method and evidence for the complete cable-tray system.
Frequently asked questions
Does GI specify the steel grade?
No. It is not enough to define the substrate, thickness or coating requirement. Provide the actual material specification for the tray product.
Are pre-galvanized and post-galvanized trays the same process?
No. The coating occurs at different stages and creates different manufacturing and inspection interfaces. State the intended route explicitly.
Does the roll former include galvanizing?
Not unless that equipment is specifically included. A tray-forming line and a post-fabrication coating facility are separate scopes.
Can stainless trays use the same setup?
Only after a material and tooling review. Similar thickness does not establish equivalent forming behavior or final accessory clearances.
What should be sent for quotation?
Send the tray section, patterns, size matrix, grade, thickness, coating route and accessory references. Identify final inspection and packaging requirements so the complete delivered product is understood.
Define galvanized tray as a complete material-and-process choice
A useful GI tray proposal connects the coating route to forming, edges, accessories and traceability. That avoids treating a familiar material abbreviation as a substitute for a controlled product specification.

Continue your research
- Cable Tray Roll Forming Machines
- Cable Tray Roll Forming Machine
- Cable Ladder Roll Forming Machine
- Solid Bottom Cable Tray Roll Forming Machine
- U Channel Cable Tray Roll Forming Machine
- Cable Support Channel Roll Forming Machine
- How Cable tray roll forming machine Works
- How To Choose a Cable tray roll forming machine
- Cable tray roll forming machine Price: What Affects the Cost?
Configuration & specification inputs
Match the configuration to your section drawing, material and production requirements.
| Parameter | Requirement / confirmation needed |
|---|---|
| Profile geometry | Approved galvanized-tray section, solid or perforated pattern, top returns and connection details. |
| Material | Explicit steel grade and pre-galvanized or post-fabrication galvanizing specification. |
| Thickness & grade | Base-metal thickness convention paired with grade, coating and tray dimensions. |
| Process route | Specified coated or uncoated input, feature making, tray forming, cutting and defined final surface processing. |
| Cutting | Tray lengths and edge condition coordinated with the required delivered protection route. |
| Output | Accepted final-condition tray orders with material, size and pattern changes stated. |
| Electrical supply | Utilities for tray fabrication; any separate galvanizing equipment explicitly outside or inside scope. |
| Acceptance | Material identity, geometry, patterns, coated surfaces, edges, covers, couplers and final bundle reference. |