
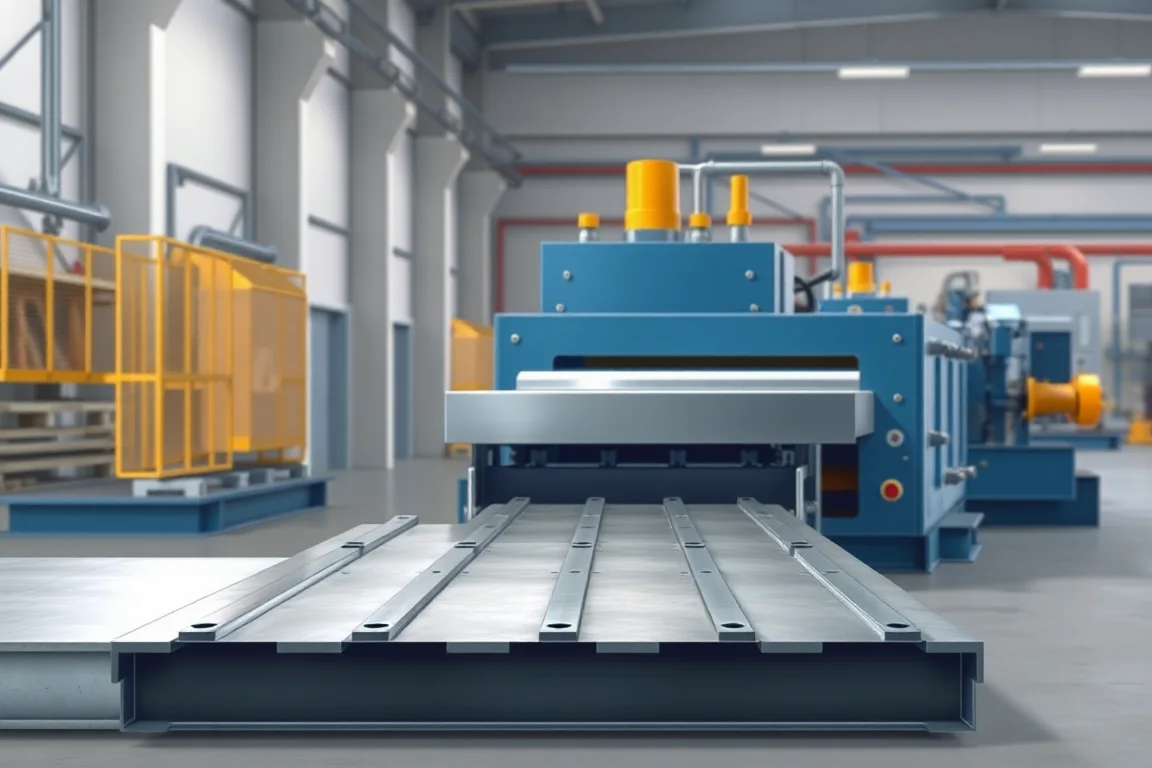
A scaffold plank roll forming machine produces the individual walk board that spans between two supports on a scaffold structure. It does not build a full deck or platform assembly. The machine takes structural steel strip through a sequence of driven rolls that progressively bend the strip into a closed or open plank profile, then cuts it to length and prepares the ends for whatever connection the scaffold system uses. The finished part is a single plank: a walking surface with side returns, often some form of perforation or embossed texture, and an end detail such as a hook, end plate or punched hole pattern.
Buyers often confuse this machine with a deck panel line. The useful distinction is the delivered component and assembly scope, not an assumed width or material-weight ranking. This page concentrates on the individual plank body and its end connection; a complete deck project may include additional frames and assembly operations. If you are forming planks, the process route in the selection data applies directly: punch or emboss, form the plank or channel, cut off, then fit or join the end attachment, then inspect.
What the plank forming machine supplies
A plank roll forming machine supplies a shaped steel body cut to a controlled length, with the walking surface, side returns and any drainage or traction features formed in the same pass sequence. The equipment scope normally includes a decoiler, a strip feed and guide section, a punch or emboss station where the strip is still flat, a series of forming stands, a cutoff press, and a runout or stacking arrangement. The end connection may be formed into the plank itself, punched into the ends, or added as a separate fitting after cutoff, depending on the scaffold system.
The selection data makes one point explicit: include anti-slip features and the hook or end-plate joining operation in the equipment scope. A quotation that stops at the cutoff press and leaves the end attachment to a separate manual operation is not quoting the same finished product. When you compare quotations, compare the same finished-plank scope. A mill that forms beautifully but delivers planks with unfinished ends has simply moved the bottleneck downstream.
Thickness and grade are buyer-specified and require supplier verification against the actual strip you intend to run. The machine operating range is a property of the tooling and drive design, not something a buyer should assume from a general description. State the base-metal thickness and grade you intend to use, and ask for confirmation that the forming stands, punch tooling and cutoff can handle the full range without marking or edge cracking.
Walking surface and side-return drawing
The walking surface is the part of the plank a person steps on, so its drawing controls most of the tooling cost. A typical formed plank has a flat or lightly ribbed walking surface, two side returns that turn down or up to stiffen the section, and often a small hem or lip at the edge of each return. The side-return radius, the return height, and any hem all require their own forming passes. Tight radii in thick strip are the hardest combination, because the outer fibers of the bend stretch and the inner fibers compress; if the radius is too tight for the grade and thickness, the surface can craze or crack.
The drawing also sets the overall plank width and the crown or camber of the walking surface. If the approved design specifies a crown, reproduce it consistently and assess its relationship to drainage, mating interfaces and stacking; do not add or change a crown as an assumed performance improvement. Ask how the drawing dimension is controlled: whether the forming stands are adjusted by shim, by screw, or by a combination, and whether the last stands are used as sizing stands to bring the finished section to the drawing tolerance.
Side returns affect more than stiffness. They set how the plank nests with adjacent planks, how it sits on a bearer or hook, and how easily the surface can be cleaned. Compare a plain formed plank body, which is a single strip bent into a walkable channel with returns, against an assembled plank, in which the walk surface is one piece and separate side members or end brackets are attached by welding, riveting or fasteners. Forming the whole body in one strip reduces secondary joining and gives more consistent geometry, but it limits how complex the returns can be and demands more forming stands. The assembled approach allows thicker or different edge members, but adds handling, fixture and joining labor, and introduces joint quality as a variable.
Perforation or embossed traction features
Traction features on a plank are usually one of three kinds: punched holes or slots in the walking surface, embossed dimples or a raised pattern, or a combination of both. Punching removes material and creates openings that also drain water and debris. Embossing displaces material without removing it and produces a raised texture that can improve grip while keeping the surface closed. Each approach has different tooling and process implications.
Punched holes are made in a press station while the strip is still flat, before forming. This is the normal sequence because flat strip is easier to locate and the punch tools are simpler. The hole pattern must be registered to the cutoff length so the pattern repeats correctly plank to plank and so the holes do not land in a bend radius, where they would distort. Embossing is also usually done flat, with a patterned die set that displaces the strip; the displaced material must not thin the section below what the specification allows.
The critical question is whether the traction feature is created before or after forming. Features made after forming require a second press or an inline station aligned to the formed section, which is more complex and can mark the finished surface. Features made before forming must survive the subsequent bends without tearing at the hole edges. If you want holes close to a side return, expect the supplier to check the bend line against the hole pattern. No claim about slip resistance should be assumed from the presence of a texture; the manufacturer of the scaffold system is responsible for qualifying the finished plank for its intended use.
Material and finish requirements
Planks are normally formed from specified structural steel strip with the required finish and joining procedure. The finish may be bare, oiled, painted, or galvanized, and the choice affects the line. Pre-galvanized or coated strip can be formed, but the coating must survive the bends without flaking, and the tooling must be kept clean to avoid coating buildup. Post-forming galvanizing is common on planks because the cut ends and punched holes expose bare steel; if the plank is to be hot-dip galvanized after forming, the drawing must account for drainage and venting so the coating reaches all surfaces and does not pool in closed returns.
Joining procedure matters when an end fitting is welded or riveted to the plank. Welding a fitting to a formed plank introduces heat that can distort the walk surface and destroy a coating locally. Riveting or bolting avoids heat but requires accurate hole alignment between the plank and the fitting. Both approaches require the equipment scope to include the joining operation or a clearly defined fixture for it. State the finish and joining procedure in the selection data and confirm that the proposed line supports it.
Punching and forming sequence
The standard sequence for a plank line is punch or emboss first, then form, then cut off. Punching flat strip allows a compact press with simple tooling and good pattern registration. After punching, the strip enters the forming stands, where the profile is built up over successive passes. Each stand makes one or two controlled bends, and the accumulated passes bring the strip to the finished section. The number of stands depends on the profile complexity: a simple channel with two returns needs far fewer stands than a section with hems, a crown and a closed return.
Roll design should keep the strip moving without excessive tension between stands. If one stand pulls harder than the next, the strip can stretch, the hole pattern can distort, and the finished length can vary. Length control is normally handled at the cutoff, but consistent forming is what makes the cutoff predictable. Ask whether the line uses a loop or dancer between the decoiler and the first stand to isolate strip tension, and how the forming speed is synchronized with the punch and cutoff so the pattern stays in register.
Inspection points belong inside the sequence, not only at the end. A first-piece check after the punch station confirms hole position on flat strip; a check after the final forming stand confirms the section; a check after cutoff confirms length and end quality. A line that only inspects the finished stack hides where a fault was introduced.
Cutoff and end-connection operations
Cutoff requirements should be confirmed as profile-supported cutoff, cut lengths, end quality and any secondary operations. A plank cutoff usually uses a shear or a die that cuts the formed section cleanly without crushing the returns. Cutting a formed profile is harder than cutting flat strip because the die must match the section and support the walls during the cut. A crushed or burred end is not just cosmetic; it can interfere with the end connection and with stacking.
The end connection is where plank lines differ most from general roll forming lines. Some scaffold systems use a hook formed into the plank end that engages a bearer or ledger. Others use a flat end plate with punched holes for bolts or pins. Others use a separate casting or forging attached to the plank. A hook made locally at the leading or trailing end needs a specified end-forming or secondary operation. Longitudinal roll passes alone do not create such discrete end-hook geometry; coordinate cutoff and end forming in the supplied route. If the end is punched, the punch station must handle the end pattern, which may be different from the walking-surface pattern and may require a separate tool or a second station.
When the end fitting is a separate part, the line scope must include the fitting operation, the fixture that holds the plank and fitting in alignment, and the inspection that verifies the finished end. It is common for a quotation to cover the forming and cutoff but to leave the fitting to the buyer; that is a legitimate division of scope as long as both sides know it. Compare the same finished-product scope across quotations so the price difference reflects the actual work.
Variants, tool changes and first-good-plank recovery
A plank line can be built for a single fixed profile or for changeover between several plank variants. Variants may differ in width, return height, hole pattern, end style or length. Changing width or return geometry usually means changing forming rolls or at least some roll sets, which is a substantial tooling change. Changing hole pattern may only require changing the punch tool. Changing length is normally a cutoff and control adjustment and is the easiest changeover.
Ask how changeover is structured. Tooling that is keyed and pre-set on a cart can be swapped faster than tooling that must be adjusted stand by stand. Digital controls that store recipes for each variant reduce setup errors. The practical test is how many planks are scrapped before the line produces a first good plank after a change. That number, and the time it takes, is a real production cost that should be discussed before purchase, not discovered afterward.
First-good-plank recovery is a discipline as much as an equipment feature. After a changeover, trained personnel should follow the approved first-part and safe adjustment procedure, verifying section, features, length and end condition before releasing the new setup. Skipping this step to save time usually produces a pile of marginal planks that must be reworked or scrapped.
Surface and edge condition and safe handling
Formed and cut steel has sharp edges, burrs and, on coated strip, exposed cut faces. The line should control burrs through the approved punching and cutoff tooling condition, cutting settings and profile support, but planks still require safe handling from the runout to the stack. Handling equipment, gloves, edge protection and controlled stacking are part of the production environment, not optional extras.
Surface condition also matters for the finished product. Roll marks, scuffing from the runout table and coating damage from poor handling all reduce the plank's appearance and can affect corrosion performance at damaged areas. Ask how the line protects the walking surface after forming, whether the runout uses protected rollers or belts, and how planks are stacked without sliding one surface across another.
Inspection with controlled mating references
Inspection of a plank should use controlled mating references, not just a tape measure. A section gauge or template that matches the drawing confirms the walking surface, returns and overall width. A length stop or gauge confirms cut length. A hole-position gauge or a mating fixture confirms that the end connection will fit the scaffold component it is designed to engage. The strength of this approach is that it checks the features that matter for assembly, not just the features that are easy to measure.
Keep a controlled reference set: a drawing, a gauge, and a known-good plank. When a dispute arises about whether a plank is acceptable, the reference set settles it. Inspection records should identify the plank variant, the gauge used and the measured features. No acceptance decision should rely on a claim about load capacity or safe use; those are manufacturer-qualified system requirements, and the plank line's job is to produce the geometry and condition the drawing specifies.
Accepted plank output and bottlenecks
Define accepted output per shift with the actual profile and material, and count the full route through forming, cutting, attachments, inspection and handling. An efficient mill can still be constrained by an omitted assembly operation. If the end fitting is done manually, that station may set the real rate. If inspection is thorough and slow, inspection may be the constraint. If planks must be stacked by hand, handling may be the constraint.
The useful exercise is to list every step from coil to packed plank and estimate its rate. Suppose, hypothetically, forming and cutoff can produce a plank every few seconds, but a single manual fitting station can only complete a fraction of that number per hour. The line output is then the fitting rate, not the mill rate. Adding a second fitting station or automating the fitting may be more valuable than increasing forming speed. Numerical targets should be based on a real time study of the actual route, not on assumptions.
Quotation and acceptance checklist
Use a checklist that mirrors the selection data so nothing is left implicit. The following items are the minimum to resolve before purchase:
- Profile and drawing: walking-surface geometry, side returns, hems, crown, overall width and tolerances.
- Material: structural steel specification, finish, and joining procedure.
- Thickness and grade: base-metal thickness and grade range, verified by the supplier against the proposed tooling.
- Process route: punch or emboss, plank or channel forming, cutoff, end fitting or joining, inspection.
- Cutoff: profile-supported cutoff, cut lengths, end quality, secondary operations.
- Output: accepted planks per shift for the actual profile and material, including attachments and inspection.
- Power: voltage, frequency and phase stated by the buyer, with installed power from a confirmed equipment schedule.
- Acceptance: the full route through forming, cutting, attachments, inspection and handling, compared on the same finished-product scope across quotations.
During acceptance, run the agreed profile and material, use the controlled references, and record the results. Confirm changeover time and first-good-plank recovery if more than one variant is purchased. Confirm that the end connection fits its mating component. Confirm that handling and stacking are safe and that the surface condition meets the drawing. Only then sign off.
Frequently asked questions
Can one scaffold plank roll forming machine produce both plain and assembled planks?
A line can form the plank body for either approach, but the assembled plank adds separate side members or end brackets that require fixtures, joining equipment and inspection. If you intend to sell assembled planks, the equipment scope must include that joining operation or a clearly defined manual station. A forming line quoted without it is only part of the production route.
Should traction holes or embossing be made before or after forming?
Pre-forming feature production can simplify access to flat strip, but the suitable sequence depends on the drawing, tooling and final feature condition. Features near bends need explicit development and inspection rather than a blanket assumption that every design uses the same route. If a design requires a feature after forming, it needs a dedicated station aligned to the formed section, which is more complex and can mark the surface.
How do I specify cutoff for a formed plank with end hooks?
Specify the cut length, the end condition, and whether the hook is formed in the strip or added later. A profile-supported cutoff die must match the section and must not crush the returns or cut through a formed hook. If the hook is a separate fitting, the cutoff only needs to produce a clean end that accepts the fitting, and the fitting operation becomes part of the scope.
What causes hole-pattern drift along a formed plank?
Pattern drift usually comes from strip tension differences between the decoiler and the forming stands, or from inconsistent forming speed relative to the punch and cutoff. Review feed measurement, registration, strip condition and the specified coordination between operations. A buffer or synchronized drive arrangement must be validated for the actual pattern; it does not by itself guarantee registration. Regular first-piece checks after the punch station catch drift before a full run is affected.
How should I evaluate output claims for a plank line?
Count the full route through forming, cutting, attachments, inspection and handling, using your actual profile and material. An efficient mill can still be constrained by a manual end-fitting station. Ask for the assumption behind any output figure, and compare quotations on the same finished-product scope so the comparison reflects real work, not a partial line.
What references should be used to accept finished planks?
Use a controlled drawing, a section gauge or template, a length gauge, and a mating fixture for the end connection. Keep a known-good plank with the reference set. These references check the features that matter for assembly and use, and they settle disputes without relying on unverified claims about performance or safe use.

Continue your research
- Scaffolding Roll Forming Machines
- Scaffolding Deck Roll Forming Machine
- Scaffold Ledger Roll Forming Machine
- Ringlock Scaffold Ledger Roll Forming Machine
- Cuplock Scaffold Ledger Roll Forming Machine
- Scaffold Frame Profile Roll Forming Machine
- How Scaffolding roll forming machine Works
- How To Choose a Scaffolding roll forming machine
- Scaffolding roll forming machine Price: What Affects the Cost?
Configuration & specification inputs
Match the configuration to your section drawing, material and production requirements.
| Parameter | Requirement / confirmation needed |
|---|---|
| Profile geometry | A scaffold plank needs a walking surface, supporting ribs and end attachments. Include anti-slip features and the hook or end-plate joining operation in the equipment scope. |
| Material | Specified structural steel with the required finish and joining procedure |
| Thickness & grade | Buyer to specify base-metal thickness and grade; operating range requires supplier verification. |
| Process route | Punch/emboss → plank or channel forming → cutoff → end fitting/joining → inspection |
| Cutting | Confirm profile-supported cutoff, cut lengths, end quality and any secondary operations. |
| Output | Define accepted output per shift with the actual profile and material. |
| Electrical supply | Buyer to state voltage / frequency / phase. Installed power requires a confirmed equipment schedule. |
| Acceptance | Count the full route through forming, cutting, attachments, inspection and handling. An efficient mill can still be constrained by an omitted assembly operation. Compare the same finished-product scope across quotations. |