
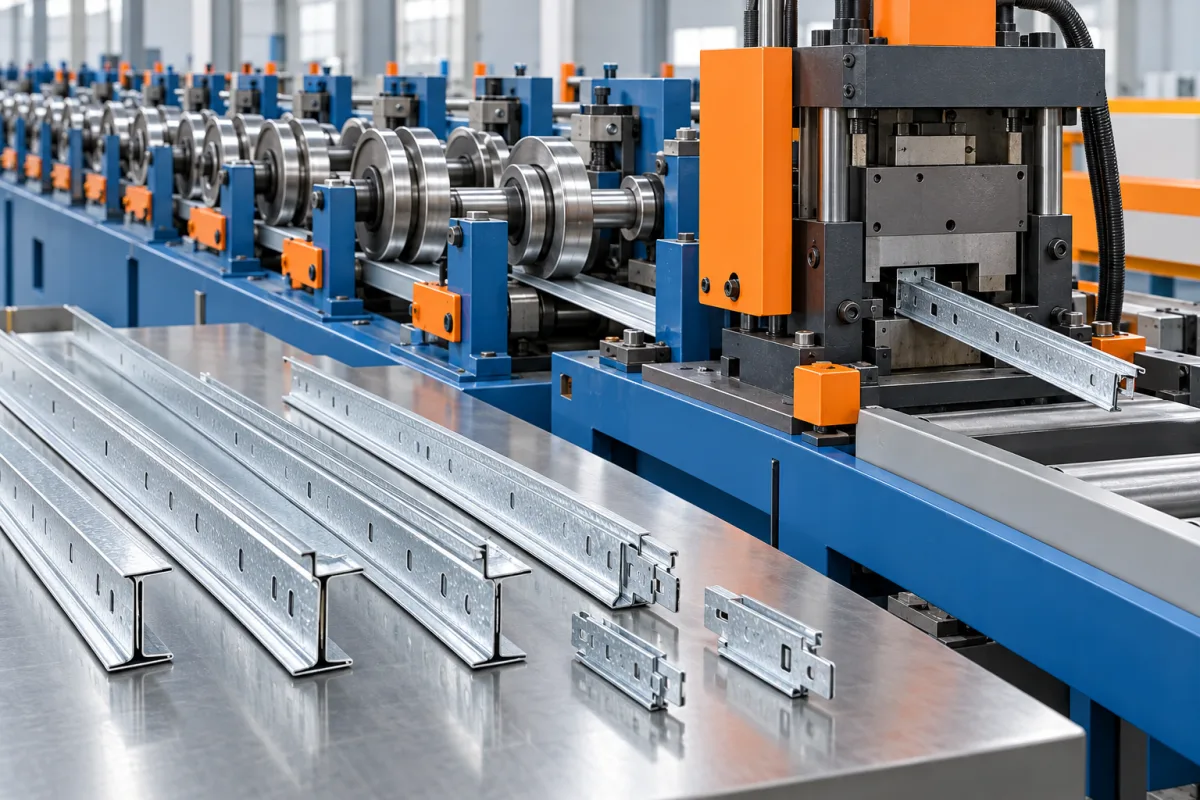
A ceiling cross T roll forming machine produces the transverse members that connect into the specified main-runner grid. The product includes more than a T-shaped body: its end connectors, length references and visible flange relationship determine whether the grid assembles at the intended module.
Cross-tee production should therefore be specified around the actual main-runner opening and connection system. A similar flange width or nominal grid size does not establish compatibility with another manufacturer's components or a different connector design.
What is the complete cross-tee product?
Define body height, visible flange, top geometry and any separate decorative cap. Show both ends, including connectors and any different left/right details. State how overall length and installed module length are measured.
Those length conventions matter because the connector extends into another member. The physical piece length may not be the same quantity used to describe the ceiling grid module. Keep both definitions explicit in drawings and inspection records.
How do end connectors determine machine scope?
The connector may be an integral feature or a separately attached component, depending on the design. The proposal should explain the forming, punching, attachment and inspection operations needed to complete it. A body former alone may leave significant downstream work.
Use the intended main-runner sample and mating cross tee during review. Some intersections require a defined relationship between connectors entering from opposite sides. That relationship cannot be evaluated by looking at one finished end in isolation.
Which dimensions control the installed grid?
- Installed module length and its reference points.
- Connector position relative to the visible flange.
- Body and flange alignment at each end.
- Any midpoint opening for another tee.
- Cap and end appearance where visible.
Specify these dimensions on the complete product rather than only on the blank body. Connector attachment or end forming can change the final relationship after the main roll-forming operation is finished.
How is the cross tee manufactured?
The route forms the body and, where used, applies or integrates the visible cap. Feature-making and end operations create the required connector arrangement, followed by length control, cutting and transfer. The exact sequence depends on the product construction.
Ask which operations occur in one coordinated route and which require a separate station. Short cross tees can create a high frequency of cutting and transfer events. The proposal should demonstrate control of the actual finished lengths rather than rely on long-body production speed.
What materials and finish need to be specified?
Identify body material, thickness and coating, plus cap material and visible finish where separate. Connector material or construction should also be defined. Different components may have different forming and appearance requirements.
Inspect the complete tee for cap alignment, edge condition and marks. Check connectors after normal handling. A clean visible face does not establish a functional end, while a strong-looking connector does not excuse a distorted exposed flange.
How should main-runner engagement be tested?
Connect cross tees into the intended openings using the specified assembly sequence. Check engagement, alignment and the visible intersection. Where opposite connectors share an opening, test the complete pair rather than only one side.
Record unexpected insertion resistance, looseness or local adjustment. Do not approve a connector by enlarging the receiving opening or substituting a different runner. The trial should represent normal parts from the intended grid system.
Can several module lengths share one line?
Potentially, but changes may involve end positioning, midpoint features, transfer timing and inspection as well as the cut program. Request a variant matrix for each finished length and connector family. Identify any tools or components that must be exchanged.
Demonstrate first-good-tee recovery after a meaningful change. Measure the installed module and assemble the intersection. A correct raw cut length is not enough if the connector relationship has not been recovered.
What should the acceptance grid include?
- Measure complete tee geometry and length datums.
- Inspect both end connectors and visible flange alignment.
- Join tees to production-intent main runners.
- Test opposite-side intersections where used.
- Check midpoint connections for shorter tees if required.
- Inspect finish and connector condition after packaging.
- Record accepted complete pieces for the actual length mix.
Keep system performance assessment separate from manufacturing fit. Load capacity, fire behavior and other ceiling requirements concern the complete approved assembly and its verification.
Frequently asked questions
Is nominal module length the same as physical length?
Not necessarily. The connector engages another member, so the drawing must define installed and physical length references separately. Use the specified measurement method for acceptance.
Can any cross tee fit a matching-width main runner?
No. Visible flange width does not define the connector and opening interface. Compare the actual components and test the intended assembly.
Are end connectors included with a body former?
Only if the equipment scope explicitly includes their production or attachment. Identify every operation needed to deliver complete saleable cross tees.
Why test two connectors entering one opening?
Where the design uses that arrangement, the connectors interact with each other and the runner. Testing one end alone cannot establish the complete intersection fit.
What should a quotation request contain?
Provide complete cross-tee drawings, main-runner references, connector construction, materials, lengths and packaging requirements. Include the expected mix of module sizes and any midpoint features.
Specify the finished intersection, not only the T body
A useful cross-tee production brief connects forming to end connectors and installed grid dimensions. That makes the machine trial a test of complete ceiling components rather than an isolated section shape.

Continue your research
- Ceiling & Furring Roll Forming Machines
- Furring Channel Roll Forming Machine
- Main Channel Roll Forming Machine
- Hat Furring Channel Roll Forming Machine
- Ceiling Carrying Channel Roll Forming Machine
- Ceiling T Main Runner Roll Forming Machine
- How Ceiling roll forming machine Works
- How To Choose a Ceiling roll forming machine
- Ceiling roll forming machine Price: What Affects the Cost?
Configuration & specification inputs
Match the configuration to your section drawing, material and production requirements.
| Parameter | Requirement / confirmation needed |
|---|---|
| Profile geometry | Complete cross-T body, visible flange, optional cap and both specified end connectors. |
| Material | Defined body, cap and connector materials with their required finishes. |
| Thickness & grade | Component-specific thickness combinations approved through forming and connector completion. |
| Process route | T-body forming, specified cap integration, end-connector operations, registered cutting and controlled transfer. |
| Cutting | Physical and installed-module lengths with explicit datums and correctly positioned connectors. |
| Output | Accepted complete cross tees for the actual module-length and connector mix. |
| Electrical supply | Utilities for body and cap forming, end operations, cutoff and short-piece handling. |
| Acceptance | Complete length, both connectors, main-runner engagement, opposite intersections and packaged finish. |