
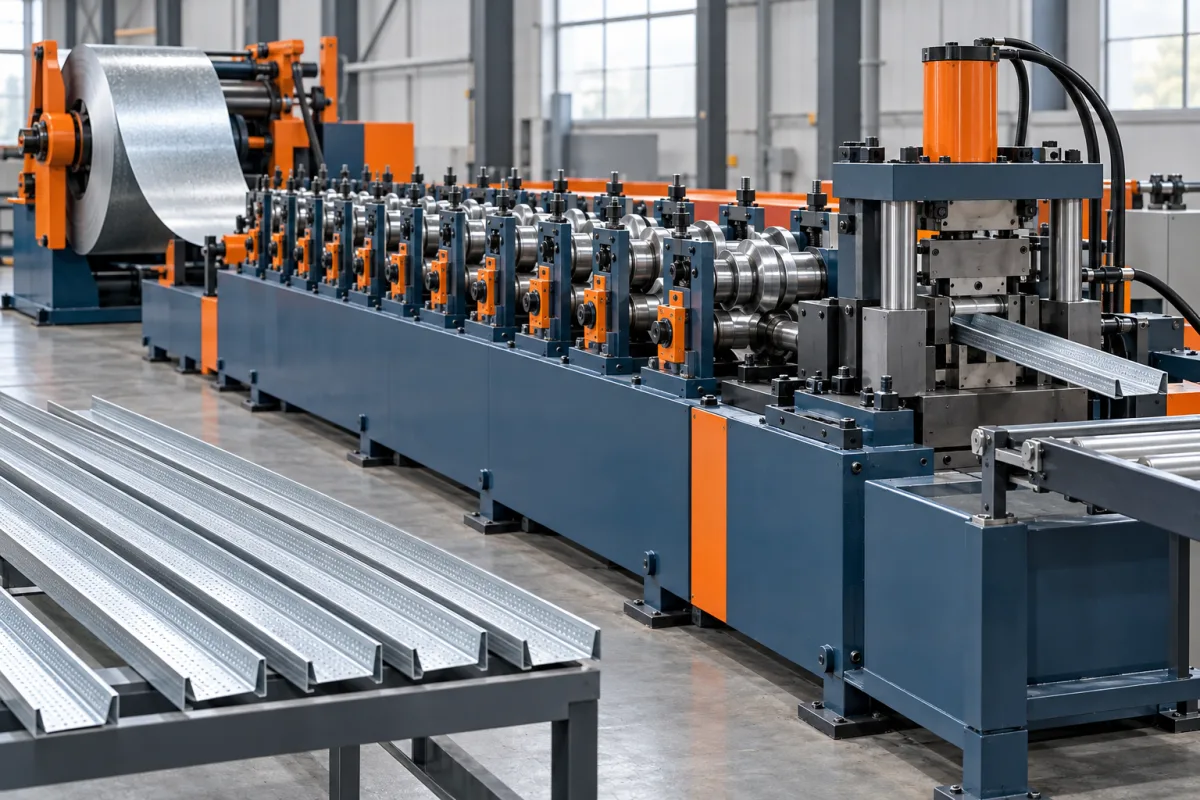
A furring channel roll forming machine produces the shaped metal members used to establish a lining or ceiling support face within a specified construction system. The product is often described as a hat channel, but that familiar outline can conceal important differences in crown width, side depth, outward flanges and clip engagement.
The equipment should therefore be selected around the complete furring assembly. A channel fixed directly to a substrate, a channel clipped to a main carrier and a resilient acoustic channel are not interchangeable simply because all can sit behind a board lining. Their drawings and functions lead to different forming and inspection requirements.
Which furring product is being manufactured?
Start by identifying how the channel is attached and which surface carries the lining. A typical hat-shaped member provides a raised face with outward feet, while a Z-shaped furring member has a different offset and fastening arrangement. Proprietary clip-on channels can include returns or edges that govern engagement.
A resilient channel is a separate engineered product whose performance depends on its specific geometry and installation within an assembly. Do not describe an ordinary furring channel as acoustically equivalent merely because it creates a gap behind the board. If resilient products are required, include them as separately defined sections.
What should the section drawing establish?
The drawing needs to show the lining face, overall depth, side angles, outward flanges and any hems or returns. Identify the functional dimensions used by clips or other connectors. A simple overall width can be insufficient where a connector engages only a narrow part of the edge.
- Crown: the face width and geometry available for the specified lining attachment.
- Stand-off: the distance and section shape establishing the intended offset.
- Feet: flange widths, fastening references and edge condition.
- Engagement: clip contacts, returns or other mating features.
- Finished member: length, straightness, twist and acceptable cut ends.
Provide the mating clip or carrier drawing and samples where applicable. Approving the channel in isolation leaves the most important assembly question unresolved.
How does the line develop a furring channel?
The strip is guided from the coil into a sequence of forming passes that develop the crown, sides and feet. Any specified stiffening, holes or edge details must be included in the route. Cutting and collection then need to preserve the geometry that allows the channel to sit or clip into place.
- Present the identified coil to the line in the required orientation.
- Guide the strip and perform any included feature-making operations.
- Develop the main bends progressively while maintaining the intended crown and flange relationship.
- Complete returns or hems where the drawing requires them.
- Cut the specified lengths with suitable support for the section.
- Collect and inspect members without flattening their raised shape or spreading their feet.
Ask the equipment supplier to explain where the functional clip edge is controlled. The final profile depends on the pass sequence and material response, not only the appearance of the last set of rolls.
How should material and surface requirements be specified?
State grade, base-metal thickness, coating and input width for each section. A narrow accessory can still require careful material control because small shape changes may affect clip fit or the lining face. Thickness alone does not describe the complete forming requirement.
Identify any surface that must remain suitable for the intended fastening or finish. Inspect coating condition at bends and contact areas after forming and normal handling. If the catalogue includes more than one material, test representative combinations rather than assuming that identical nominal thickness means identical behavior.
Record incoming coil identity with accepted sample dimensions. This is useful when a later batch appears more open, twisted or difficult to engage: the team can compare both material and setup instead of correcting the tools without evidence.
Dedicated tools or a multi-accessory production system?
A dedicated furring route can suit sustained demand for a stable section family. A multi-accessory arrangement may also produce angles, channels or other lining profiles using separate configurations. Its flexibility depends on the physical tools and change process, not the breadth of the product names in a sales list.
Request a matrix showing which dimensions adjust, which sections require another tool set and which cutoff or guide parts change. The transition between two crown widths can be different from the transition between hat and Z furring. Demonstrate the changes the business expects to make regularly.
Include the first accepted product in changeover timing. A rapid tool movement is useful only if the recovered crown, feet and clip interface meet the drawing without prolonged correction.
Why does the clip interface need an assembly trial?
A clip may depend on edge thickness, return angle, opening or the position of a small contact surface. Measuring only the channel's overall width can miss the actual reason it will not engage. Use the intended connector and the specified assembly method during approval.
Check several positions along production-length members, including near cut ends. Record resistance, looseness and any need for local reshaping. A single short sample that has been manually adjusted is not a reliable demonstration of repeatable production fit.
The assembly trial confirms manufacturing compatibility within the chosen system. It does not determine hanger spacing, allowable loads or acoustic performance. Those belong to the relevant system design and should not be inferred from an easily snapped-together sample.
What affects the lining face and installed alignment?
The crown must provide the intended attachment face, while straightness and twist influence how repeated members align. Inspect the section under consistent support conditions and identify whether a deviation exists before or after collection. Thin profiles can be altered by handling even when they leave the tools acceptably.
Where stiffening ribs or embossed features are specified, check their effect on the usable fastening surface and mating components. They should match the product drawing rather than be added as an assumed improvement. More visible features do not automatically make a channel more suitable for its intended assembly.
How should cutoff and nesting be reviewed?
The cutting arrangement should leave ends that can be handled and assembled without unacceptable flare or crushing. Inspect both feet and the raised crown after cutoff. Different section depths or returns may require corresponding support or cutting components.
For nesting, define the orientation and bundle size. Channels that nest tightly can be efficient to transport but should remain separable without damage. Check the finished bundle after normal packing pressure and movement, not only before it is strapped.
Separate similar sections by clear labels. A clip-compatible variant and a plain hat channel can look alike when bundled, so size, material and product reference should remain visible to the warehouse and customer.
What should practical output include?
Evaluate accepted lengths and completed bundles for a representative order. Cutting frequency, profile changes, coil changes and collection can govern the result. A high strip speed on a long uninterrupted run does not show how the line performs on several short accessory orders.
Compare quotations with equivalent scope: payoff, all required roll tools, feature equipment, cutoff parts, collection, gauges and commissioning. If a multi-profile package is proposed, identify what must be purchased for future accessories and how those additions affect the existing production route.
How should common deviations be investigated?
Describe the symptom first. A foot that does not sit flat, a clip edge that will not engage and a twisted member are different observations. Measure the relevant functional geometry and compare it with the accepted sample before changing a convenient roll position.
Track whether the issue follows a coil change, tool change or handling operation. Keep forming marks separate from scratches introduced during stacking. Physical inspection and correction should use the equipment maker's procedures, with authorized personnel and the required isolation.
What belongs in an acceptance checklist?
- Controlled channel and mating-component drawings.
- Representative material combinations and ordered lengths.
- Crown, side, flange, return and end measurements.
- Clip or fixing-interface checks using the intended components.
- Straightness and twist inspection under defined support.
- A required profile change followed by accepted recovery.
- Nesting, packing, identification and accepted-output records.
Retain the setup and assembled reference samples. They help operators recognize a meaningful change in the product rather than relying on memory of how the channel once looked.
Frequently asked questions
Is every furring channel a hat channel?
No. The term covers several support arrangements, including hat and offset forms. Specify the actual cross-section and attachment method. A category name cannot establish tooling or connector compatibility.
Can ordinary furring replace resilient channel?
Do not assume equivalence. Resilient products belong to a defined assembly and installation method. Their performance cannot be transferred to a different profile merely because both support a lining.
Can one line make wall and ceiling furring?
It can where the required sections and material combinations are covered by the configuration. Review the actual drawings and interfaces; the installation location alone does not prove either sameness or difference in tooling.
Why does a clip fit one batch but not another?
Compare the channel's functional edge, material and setup with the accepted reference, and confirm the clip itself. Overall width alone may miss the critical change. Avoid uncontrolled reshaping to force a fit.
Should packing be tested during acceptance?
Yes, if packed bundles are the saleable output. Nesting and strapping can alter thin sections or make them difficult to separate. Include normal handling so the trial represents the product delivered to customers.
What should an enquiry include?
Send the section and connector drawings, material range, lengths, feature requirements and expected order mix. Add nesting and bundle details. This makes the proposal specific to the furring system being manufactured.

Continue your research
- Ceiling & Furring Roll Forming Machines
- Main Channel Roll Forming Machine
- Ceiling T Grid Roll Forming Machine
- Hat Furring Channel Roll Forming Machine
- Ceiling Carrying Channel Roll Forming Machine
- Ceiling T Main Runner Roll Forming Machine
- How Ceiling roll forming machine Works
- How To Choose a Ceiling roll forming machine
- Ceiling roll forming machine Price: What Affects the Cost?
Configuration & specification inputs
Match the configuration to your section drawing, material and production requirements.
| Parameter | Requirement / confirmation needed |
|---|---|
| Profile geometry | Crown, side depth, outward feet and specified clip-engagement returns |
| Material | Specified accessory grade, coating and input-strip condition |
| Thickness & grade | Approve thickness with the intended section and connector combination |
| Process route | Guided coil, required features, crown and foot forming, edge completion and supported cutoff |
| Cutting | Preserve raised crown, feet and clip edges through cutoff and collection |
| Output | Accepted nested bundles with verified clip fit and undamaged sections |
| Electrical supply | Confirm utilities for the selected dedicated or multi-accessory arrangement |
| Acceptance | Measure functional edges, assemble intended clips, check long-member alignment and inspect packed bundles |